Buy 40ft x 8ft Raised Bunded Store for Industrial Safety
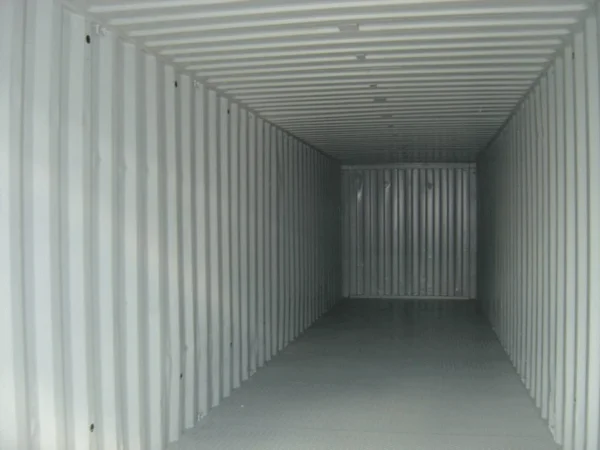
When you need to buy 40ft x 8ft raised bunded store solutions for your industrial facility, choosing a unit that guarantees maximum containment, regulatory compliance, and rugged durability is paramount. At AVE Storage Container LLC, we engineer heavy-duty industrial storage systems designed to safeguard your hazardous materials, chemicals, oils, and flammable liquids against accidental spills, leaks, and environmental contamination.
In today’s highly regulated industrial landscape, environmental protection agencies and occupational safety administrations enforce strict guidelines regarding the handling and storage of hazardous substances. Failing to meet these mandates can result in severe financial penalties, operational shutdowns, and catastrophic environmental damage. Investing in a heavy-duty buy 40ft x 8ft raised bunded store option from our premium inventory provides your business with peace of mind. Our units feature integrated, elevated containment sumps that isolate spilled liquids away from stored inventory, protecting both your workforce and local ecosystems.
This comprehensive product guide explores the structural engineering, compliance benefits, operational advantages, and technical specifications of our flagship 40-foot raised bunded chemical containers. Whether you operate in oil and gas, manufacturing, agriculture, pharmaceuticals, or logistics, read on to discover why partnering with AVE Storage Container LLC is the smartest investment for your containment infrastructure.
Why Choose a 40ft x 8ft Raised Bunded Store for Hazardous Materials?
Industrial operations generate and utilize vast quantities of chemicals, lubricants, paints, and solvents. Managing these substances safely requires more than standard warehousing. When you buy 40ft x 8ft raised bunded store units, you are acquiring a specialized containment vessel engineered to withstand harsh weather, corrosive substances, and rigorous daily handling.
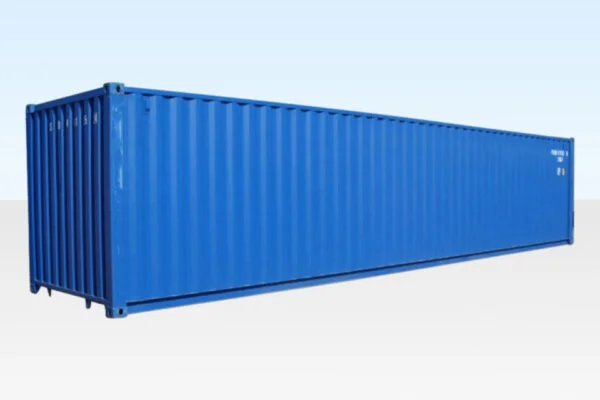
The primary advantage of a 40ft x 8ft footprint lies in its expansive storage capacity. Measuring 40 feet in length and 8 feet in width, this container offers approximately 320 square feet of floor space. This massive volume allows facilities to centralize their chemical management, housing dozens of standard 55-gallon drums, intermediate bulk containers (IBCs), and palletized goods under a single secure roof. The raised bund design elevates the storage floor above the integrated sump basin, ensuring that any leaked or spilled fluids drain safely away from stored products, preventing cross-contamination and minimizing slip-and-fall hazards for personnel.
Key Structural Features and Engineering Excellence
Every unit we supply is built to uncompromising manufacturing standards. When discerning engineers and safety managers buy 40ft x 8ft raised bunded store models from AVE Storage Container LLC, they receive a structure defined by industrial-grade resilience.
High-Grade Corten Steel Construction
Our containers are fabricated from weather-resistant Corten steel (corrosion-resistant steel). This material forms a stable rust-like appearance when exposed to the elements, sealing the surface and preventing deeper corrosion. This ensures decades of structural integrity, even in coastal environments or high-humidity regions prone to rapid oxidation.
Fully Integrated Raised Sump Basin
Beneath the heavy-duty galvanized or painted steel grid flooring lies a high-capacity liquid retention sump. Designed to comply with national and international spill containment regulations (such as EPA and SPCC guidelines), the bund captures 110% of the single largest container’s volume or 25% of the total aggregate stored volume, whichever is greater. The raised flooring guarantees that stored drums and IBC totes never sit in standing pool water or chemical residue.
Maximizing Regulatory Compliance When You Buy 40ft x 8ft Raised Bunded Store Units
Regulatory compliance is non-negotiable in modern industrial sectors. Environmental protection agencies mandate that secondary containment systems must be impermeable, chemically resistant, and capable of holding large volumes of accidental discharges.
When enterprises buy 40ft x 8ft raised bunded store infrastructure, they instantly upgrade their site audit readiness. Our containers are designed to align with stringent Occupational Safety and Health Administration (OSHA) and Environmental Protection Agency (EPA) standards. By centralizing hazardous materials within a lockable, bunded enclosure, facilities minimize their risk profile, avoiding costly citations and reinforcing their corporate commitment to environmental stewardship.
Optimal Applications and Industries That Benefit
The versatility of our large-scale containment solutions makes them indispensable across a wide spectrum of industries. Organizations routinely choose to buy 40ft x 8ft raised bunded store units for diverse operational needs:
- Oil and Gas Sector: Storing drilling mud additives, lubricants, hydraulic oils, and maintenance chemicals safely on remote drilling sites or refinery grounds.
- Manufacturing and Processing Plants: Housing solvents, cleaning agents, coatings, and production chemicals close to factory floors without violating fire or environmental codes.
- Agricultural Operations: Managing large quantities of liquid fertilizers, pesticides, and herbicides securely away from water sources and livestock.
- Construction and Infrastructure: Providing temporary or permanent secure storage for fuel additives, epoxies, resins, and hazardous job-site chemicals.
- Pharmaceutical and Chemical Industries: Keeping raw ingredients and volatile compounds contained, secure, and temperature-controlled (with optional ventilation packages).
Ventilation, Climate Control, and Safety Accessories
To ensure safe handling of volatile or temperature-sensitive substances, our containers can be customized with a variety of specialized accessories. When clients buy 40ft x 8ft raised bunded store configurations, they can request engineered enhancements tailored to their exact operational hazards.
Forced Air and Passive Ventilation Systems
Proper airflow is vital when storing chemicals that emit hazardous vapors. We offer louvered vents, mechanical extraction fans, and explosion-proof ventilation setups to prevent dangerous vapor concentrations from accumulating inside the enclosed space.
Electrical and Lighting Upgrades
For round-the-clock operations or facilities located in dimly lit yards, internal explosion-proof lighting, switchgear, and external power hookups ensure safe loading and unloading procedures at any hour of the day or night.
Durability Against Extreme Weather Conditions
Industrial storage assets must endure punishing environmental conditions, from freezing winters to scorching summers. When industrial buyers buy 40ft x 8ft raised bunded store options from AVE Storage Container LLC, they benefit from weather-tight engineering designed to repel driving rain, heavy snow loads, and high winds.
The robust corner castings, reinforced corrugated walls, and secure multi-point locking mechanisms ensure that the interior environment remains protected from moisture intrusion. This prevents moisture-induced corrosion on drum lids, container labels, and metallic packaging, ensuring your stored inventory remains in pristine condition.
Logistical Advantage: Transport, Delivery, and Placement
Transporting a 40-foot industrial container requires specialized logistics and handling equipment. At AVE Storage Container LLC, we streamline this process from initial purchase to final site placement.
When you buy 40ft x 8ft raised bunded store units through our platform, our logistics team coordinates safe, efficient delivery via tilt-bed trucks or flatbed trailers equipped with crane services. We work closely with your site managers to ensure proper ground preparation, foundation leveling, and placement alignment, allowing your facility to integrate the new containment unit into your workflow with minimal operational downtime.
Cost-Benefit Analysis: Why Investing in Quality Pays Off
While upfront capital expenditures are a key consideration for any procurement department, evaluating the long-term value of industrial containment is critical. Attempting to cut corners with substandard storage solutions often leads to catastrophic failure, regulatory fines, and expensive environmental remediation processes.
When businesses choose to buy 40ft x 8ft raised bunded store units manufactured to elite industrial standards, they protect themselves against unforeseen liabilities. The longevity of Corten steel, combined with robust secondary containment, drastically reduces asset replacement cycles and insurance premiums. It is a one-time investment that safeguards your workforce, your facility, and your corporate reputation for decades.
How AVE Storage Container LLC Ensures Quality Assurance
Quality assurance is the backbone of our manufacturing and supply chain operations. Every unit undergoes rigorous multi-point inspections before leaving our facilities. When customers buy 40ft x 8ft raised bunded store inventory from us, they receive certified weld inspections, structural load testing verifications, and epoxy coating thickness checks.
Our commitment to excellence ensures that you receive a flawless, ready-to-deploy containment vessel that meets or exceeds all structural and environmental benchmarks.
Customization Options for Specialized Industrial Needs
No two industrial facilities are identical. Recognizing this, AVE Storage Container LLC offers tailored customization services for our clients. Beyond the standard specifications, when enterprises buy 40ft x 8ft raised bunded store setups, they can request bespoke modifications.
Options include custom door placements (roll-up doors, double personnel doors, or wide cargo doors), specialized interior chemical-resistant coatings, customized sump capacities, shelving brackets, and internal partition walls to segregate incompatible chemical classes.
Comparing 40ft Storage Options Against Smaller Alternatives
Facility managers often weigh whether to purchase multiple smaller containment lockers or a single large-scale storage unit. Opting to buy 40ft x 8ft raised bunded store containers offers unmatched economies of scale.
Instead of managing numerous scattered lockers across a sprawling campus, a 40-foot unified store centralizes inventory control. This reduces auditing time, simplifies spill response protocols, streamlines forklift loading routes, and provides superior security against theft or unauthorized access to dangerous chemicals.
Best Practices for Maintaining Your Raised Bunded Store
To maximize the lifespan and performance of your containment investment, routine maintenance is essential. Once you buy 40ft x 8ft raised bunded store units and integrate them into your facility, establish a proactive upkeep schedule.
- Regular Sump Inspections: Periodically check the bunded floor basin for rainwater, debris, or accidental chemical accumulation.
- Drain Valve Management: Keep sump drain valves securely locked and sealed during normal operations, opening them only during controlled cleaning and decontamination procedures in accordance with environmental laws.
- Coating Checks: Inspect the interior and exterior painted surfaces annually for scratches or wear, applying touch-up coatings as needed to prevent rust migration.
- Seal Maintenance: Examine rubber door gaskets regularly to ensure weather-tight seals remain pliable and intact.
Frequently Asked Questions
1. What is the primary purpose when I buy 40ft x 8ft raised bunded store units?
These units are engineered for the safe, secure, and regulatory-compliant storage of hazardous chemicals, oils, and flammable liquids, featuring an elevated floor and an integrated spill containment sump.
2. How much containment capacity does the raised bund provide?
Our bunded sumps are designed to meet or exceed EPA and SPCC standards, typically capturing at least 110% of the largest single container volume stored within the unit.
3. Can I store flammable liquids inside this 40-foot container?
Yes, when equipped with proper ventilation and fire-rated electrical accessories, these units can be configured for safe storage of flammable and combustible liquids.
4. What materials are used to construct the store?
They are built using heavy-duty Corten weathering steel, renowned for its superior resistance to atmospheric corrosion and structural durability.
5. Are these units delivered fully assembled?
Yes, when you finalize your purchase, the unit is delivered fully fabricated and ready for placement on your prepared industrial pad.
6. What site preparation is required before delivery?
A level, compacted gravel pad, concrete slab, or asphalt foundation capable of supporting the weight of the loaded container is required for proper placement.
7. Can the interior be partitioned into separate rooms?
Yes, custom internal partitioning is available if you need to separate incompatible chemical classes within the same 40-foot footprint.
8. How does the raised floor protect stored inventory?
The elevated steel grating keeps drums, totes, and pallets safely above any leaked liquids or standing condensation collected in the bottom sump basin.
9. What industries benefit the most from this size container?
Oil and gas, heavy manufacturing, chemical processing, large-scale agriculture, and construction firms utilize these units extensively.
10. Are the doors secure against unauthorized access?
Yes, the units feature heavy-duty cargo doors equipped with robust multi-point locking bars and secure lock boxes to prevent theft and tampering.
11. Do you offer customization for electrical lighting?
Yes, explosion-proof interior lighting and external power distribution packages can be integrated upon request.
12. How do I maintain the sump basin over time?
Regularly inspect the basin for debris, test the drain valves, and pump out accumulated rainwater in accordance with local environmental discharge regulations.
13. What is the lifespan of a Corten steel bunded store?
With minimal routine maintenance, these heavy-duty industrial containers easily last for several decades in harsh outdoor environments.
14. Can a forklift enter the unit for loading and unloading?
The raised bund flooring is engineered to support heavy weight loads, though standard operational procedures typically utilize ramps or forklift loading at the doorway threshold depending on exact specifications.
15. How do I initiate a purchase quote with AVE Storage Container LLC?
Simply visit our product page, fill out our quick quote request form, or speak directly with our industrial sales team to discuss your exact specification requirements and delivery timeline.
Conclusion
Securing your facility’s hazardous materials management infrastructure is an investment in safety, environmental protection, and operational continuity. When you buy 40ft x 8ft raised bunded store units from AVE Storage Container LLC, you are choosing industry-leading engineering, rugged Corten steel durability, and uncompromising regulatory compliance. Centralize your chemical storage, protect your workforce, and safeguard the environment with a containment solution built to stand the test of time. Get your quote today and take the definitive step toward superior industrial safety.
Reviews
There are no reviews yet.